Manufacturing Capabilities
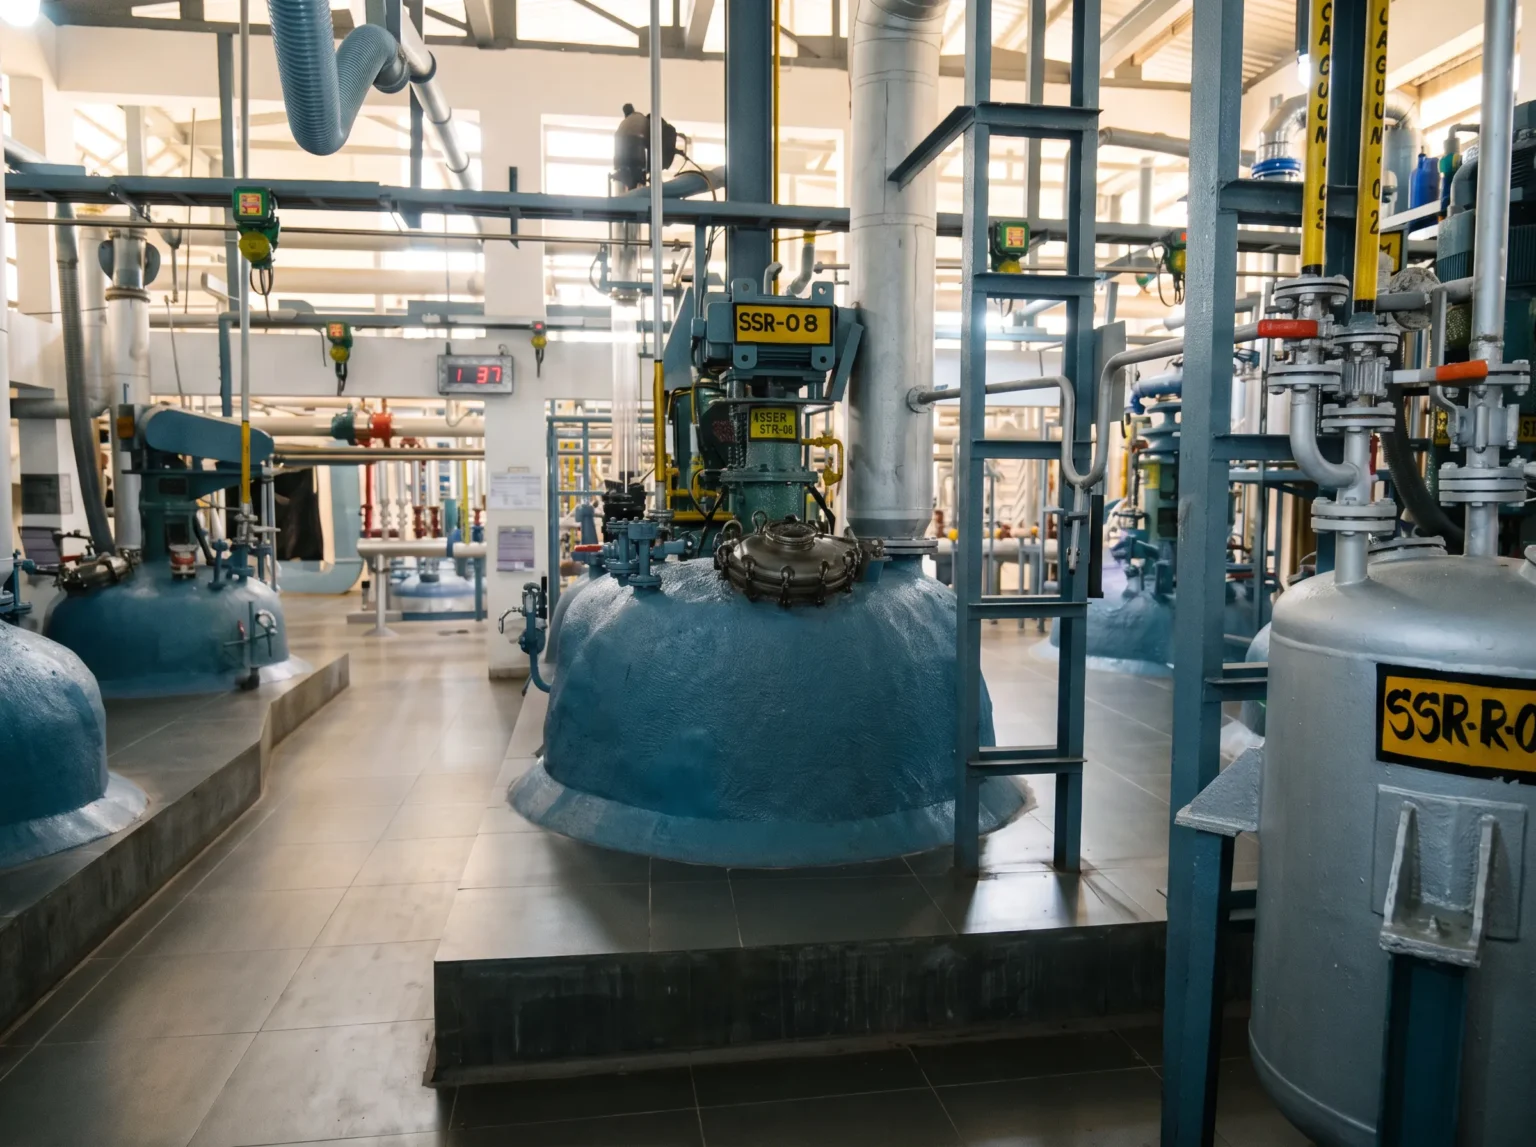
Our facilities are designed to handle a wide range of chemical processes and multistep synthesis requirements while maintaining strict process control and operational efficiency. Key capabilities include:
API Intermediate Manufacturing
Fine Chemical Manufacturing
Process Development
Process Optimization
Technology Transfer
Scale-Up Manufacturing
Pilot Batch Production
Commercial Manufacturing
Production Infrastructure
- Stainless Steel Reactors
- Glass-Lined Reactors
- Reactor Capacities from 160 L to 8000 L
- Vacuum Tray Dryers
- ANFD Systems
- Centrifuges
- High Vacuum Distillation Systems
- Material Handling Systems
- Utility Backup Systems
- Dedicated Warehousing Facilities
- Stainless Steel Reactors
- Glass-Lined Reactors
- Reactor Capacities from 160 L to 8000 L
- Vacuum Tray Dryers
- ANFD Systems
- Centrifuges
- High Vacuum Distillation Systems
- Material Handling Systems
- Utility Backup Systems
- Dedicated Warehousing Facilities
Our manufacturing infrastructure includes advanced equipment designed for safe, scalable, and efficient chemical processing. This infrastructure enables efficient manufacturing while maintaining process reliability and product consistency.
Our Core Capabilities
Advanced Chemical Manufacturing Capabilities
Multistep API Intermediate Synthesis
Contract Manufacturing
Custom Process R&D
Reaction Capabilities
Modern Production Infrastructure
Regulatory & Documentation Support
Our Products
We manufacture a broad portfolio of pharmaceutical API intermediates and fine chemicals for regulated and semi-regulated global markets.
State-of-the-Art Manufacturing Facilities
Our manufacturing facilities located in Tarapur Industrial Area are equipped with advanced production systems designed for safe, scalable, and GMP-compliant chemical manufacturing.
Advanced Processing Systems
Our core processing infrastructure is built for precision, versatility, and maximum yield.
- Stainless Steel & Glass Lined Reactors
- Reactor Capacities ranging from 160 L to 8000 L
- High Vacuum Distillation Systems
- ANFD Systems
Controlled Environments
We maintain rigorous environmental controls to ensure ultimate product purity and GMP compliance.
- Dedicated Clean Room Areas with AHU
- Vacuum Tray Dryers
- Advanced Material Handling Systems
Robust Infrastructure & Safety
A strong operational foundation ensures uninterrupted, secure, and compliant chemical manufacturing.
- Dedicated Warehousing Infrastructure
- Comprehensive Utility Backup Systems
- 24/7 Safety Monitoring Systems
Trusted by Industry Leaders
For over three decades, pharmaceutical and chemical companies worldwide have trusted Glenfin Chemicals for consistent quality, reliable supply, and technical expertise.
CANADA
Client:
- DELMAR CHEMICALS INC.
USA
Client:
- SPECGX LLC
SWEDEN
Client:
- CAMBREX KARLSKOGA AB
BELGIUM
Clients:
- BENECHIM SPRL
- PORTON EUROPE NV
CZECH REPUBLIC
Clients:
- FARMAK, A.S.
- VYZKUMMY USTAV ORGANICKYCH SYNTEZ A S.
SLOVAK REPUBLIC
Client:
- SANECA PHARMACEUTICALS A.S.
SWITZERLAND
Client:
- SIEGFRIED LTD.
SLOVENIA
Client:
- KRKA D.D. NOVO MES TO
ITALY
Clients:
- DIPHARMA FRANCIS S.R.L
- FIS - FABBRICA ITALIANA SINTETICI S.P.A.
- OLON S.P.A.
ISRAEL
Client:
- ASSIA CHEMICAL INDUSTRIES LTD
INDIA
View all 17 Local Clients
- AARTI INDUSTRIES LIMITED - CUSTOM DIVISION
- ALEMBIC PHARMACEUTICALS LTD. - GUJARAT
- ALIVUS LIFE SCIENCES LTD., ANKLESHWAR
- APITORIA PHARMA PRIVATE LIMITED
- BIESTERFELD HILDOSE SPECIALITY CHEMICALS PVT. LTD.
- CADILA PHARMACEUTICALS LTD.
- CIPLA LTD.
- COHANCE LIFESCIENCES LIMITED.
- HETERO DRUGS LIMITED
- HONOUR LAB LIMITED
- INTAS PHARMACEUTICALS LTD.
- LUPIN LIMITED
- LAURUS LABS LIMITED
- MACLEODS PHARMACEUTICALS LIMITED
- MATRIX PHARMACORP PRIVATE LIMITED
- MEGAFINE PHARMA (P) LTD
- MOREPEN LABORATORIES LIMITED
SOUTH KOREA
Client:
- DONGBANG FUTURE TECH & LIFE CO.,LTD.
JAPAN
Clients:
- CHUKAN BUTSU LTD.
- DKSH JAPAN K.K.
About Glenfin Chemicals
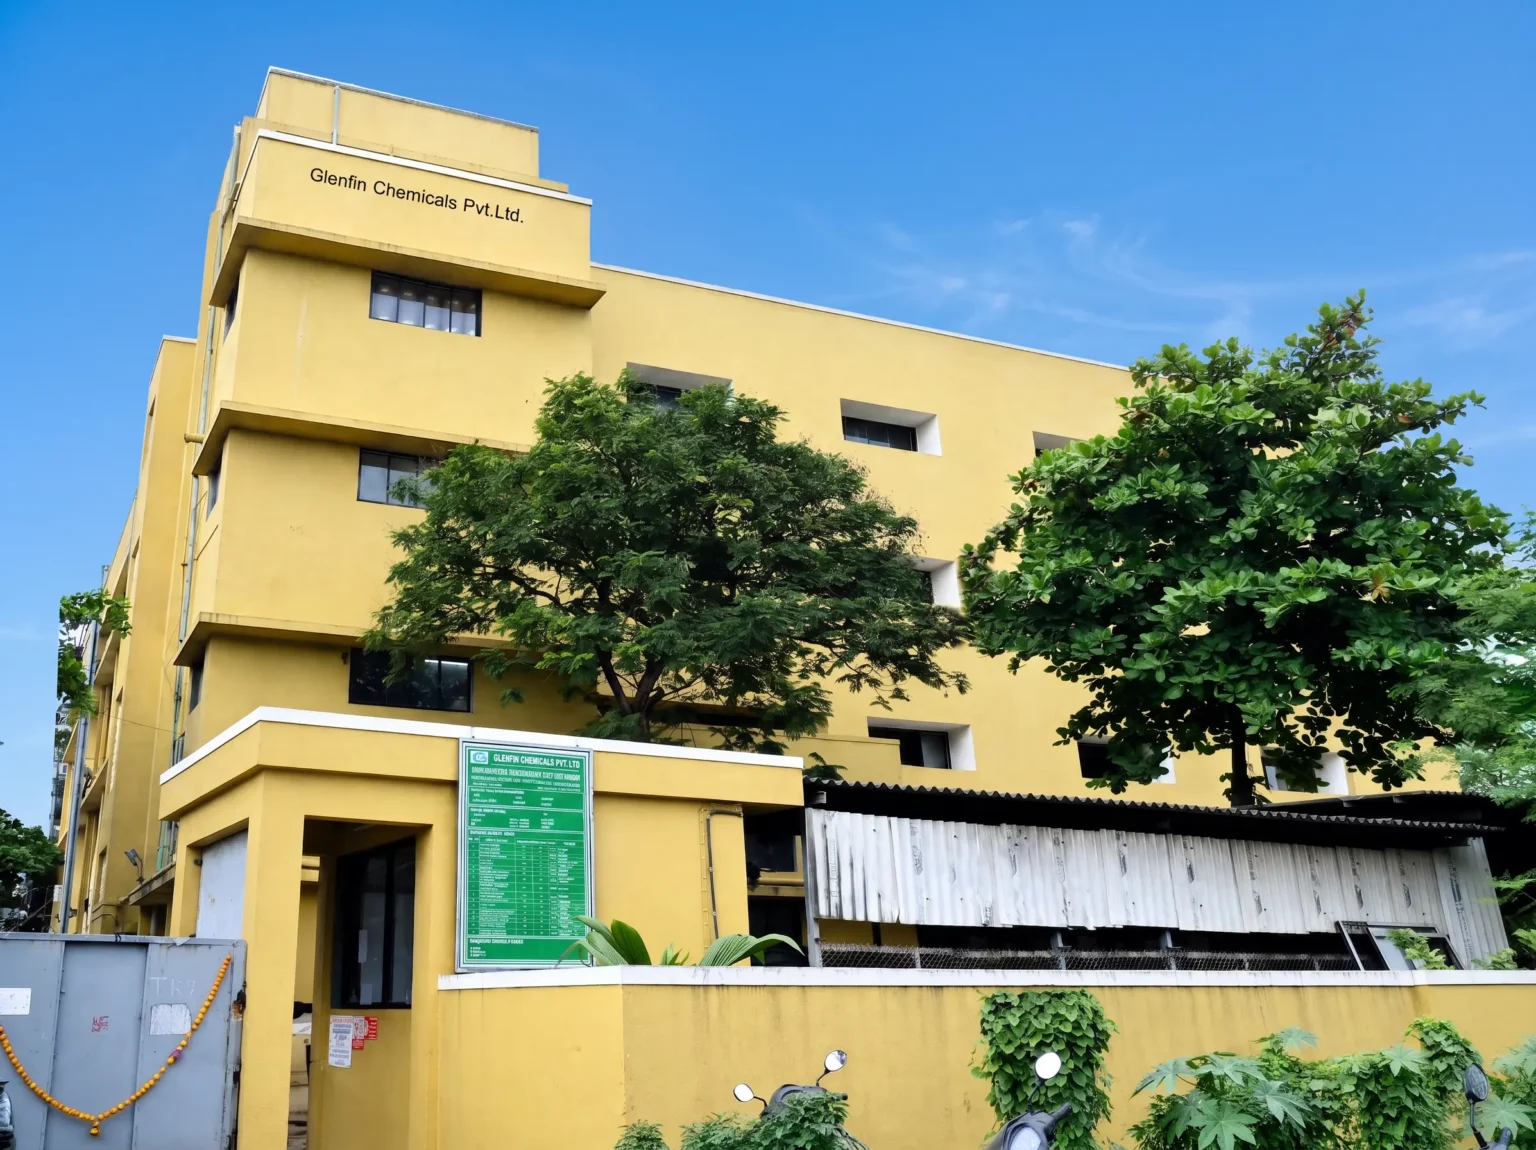
Established in 1992, the company began its manufacturing operations at MIDC Tarapur, approximately 100 km from Mumbai. Over the past three decades, Glenfin has earned a strong reputation for delivering high-quality products, technical excellence, dependable service, and long-term customer partnerships.
Our core expertise lies in the manufacturing of API intermediates, advanced intermediates, fine chemicals, custom synthesis products, and contract manufacturing solutions for both regulated and semi-regulated markets. Backed by modern manufacturing infrastructure, robust quality systems, and an experienced technical team, we consistently deliver products that meet stringent international quality standards.
With more than 30 years of industry experience, Glenfin Chemicals continues to be a trusted partner to customers across Europe, the United States, Canada, Japan, South Korea, China, and India. Our commitment to innovation, quality, and customer satisfaction enables us to support the evolving needs of the global pharmaceutical and specialty chemicals industries.